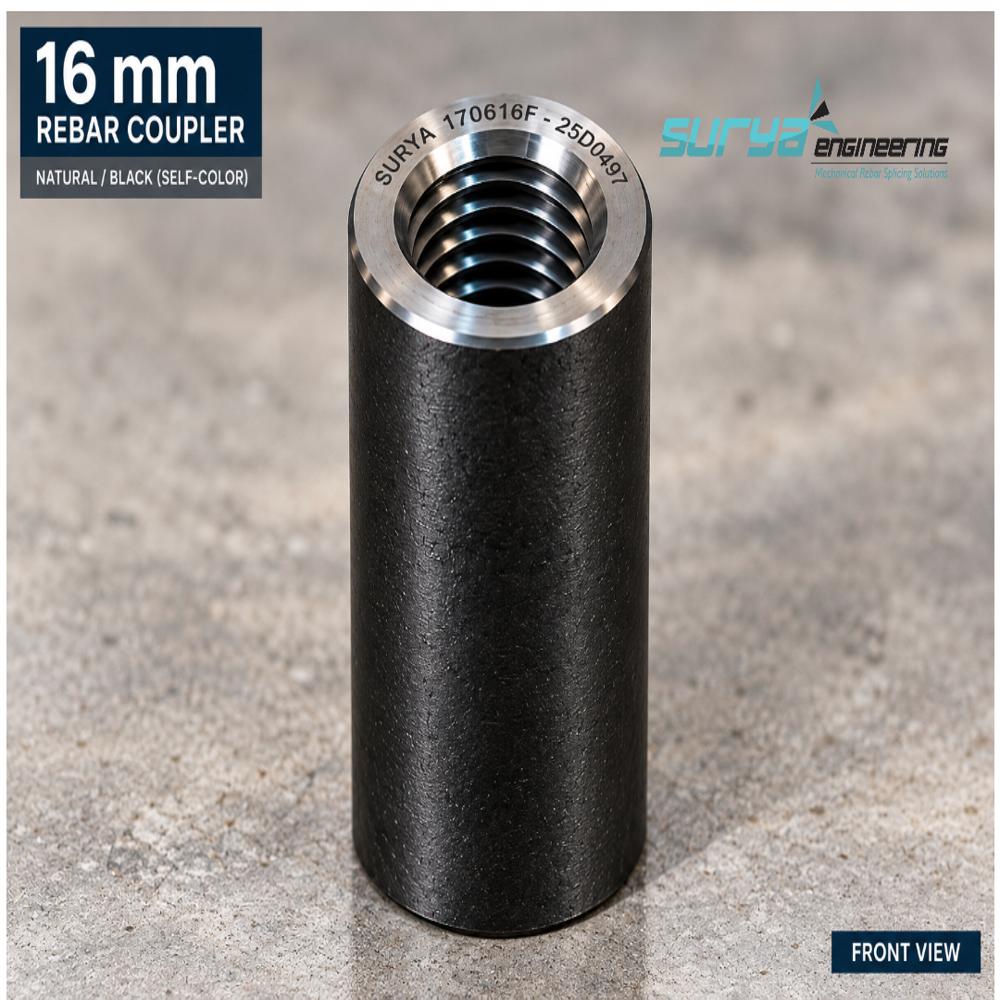
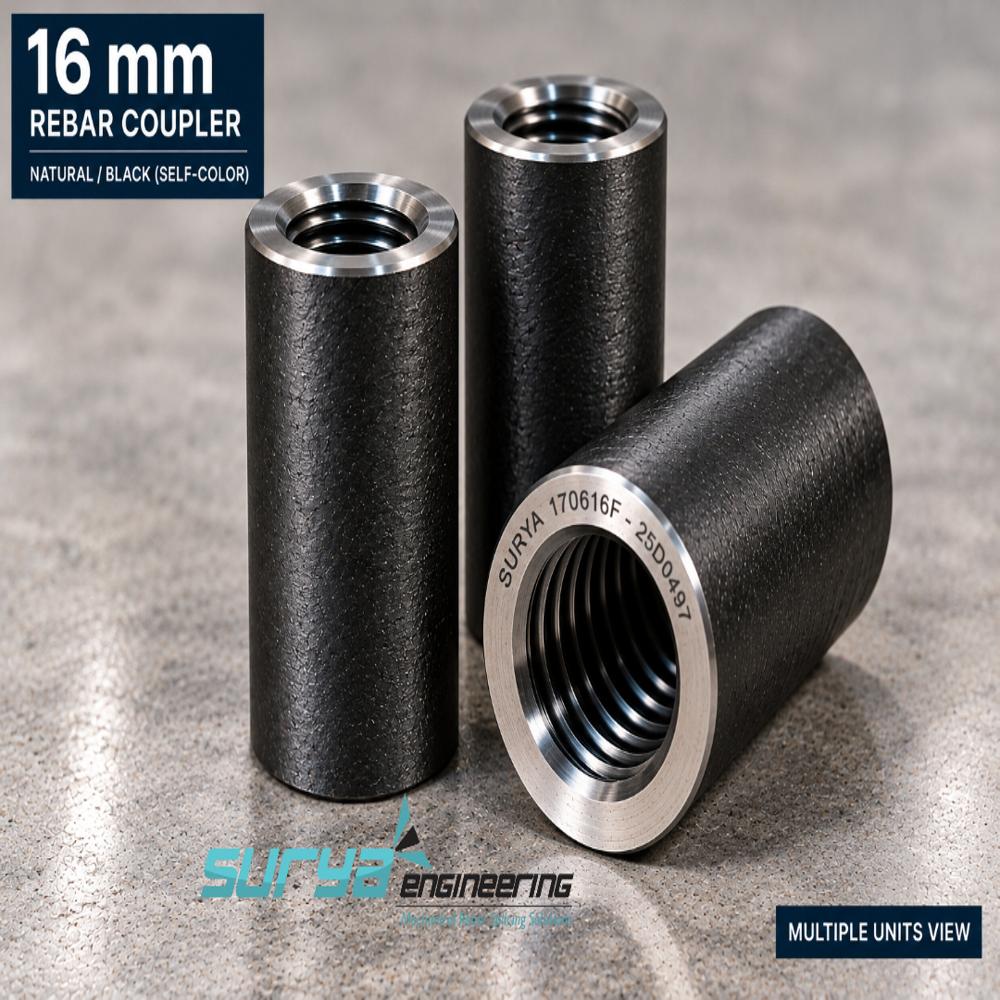
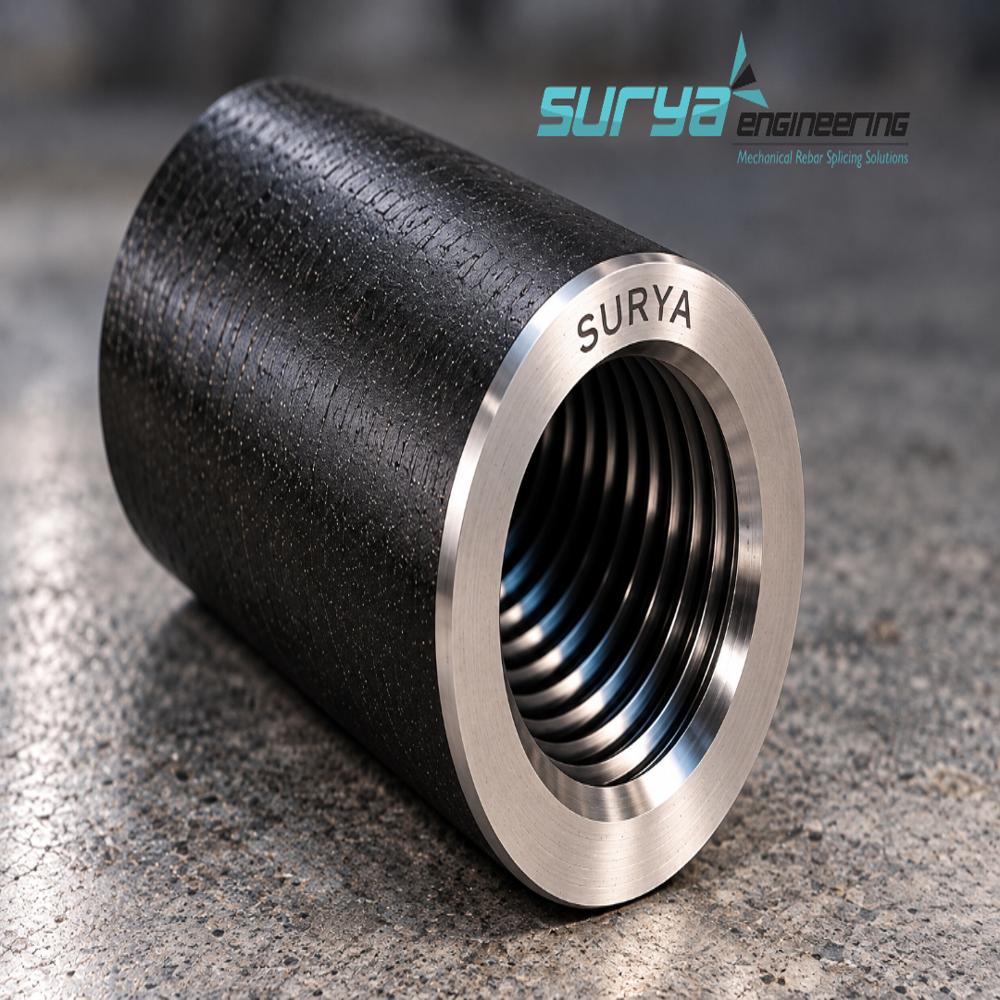
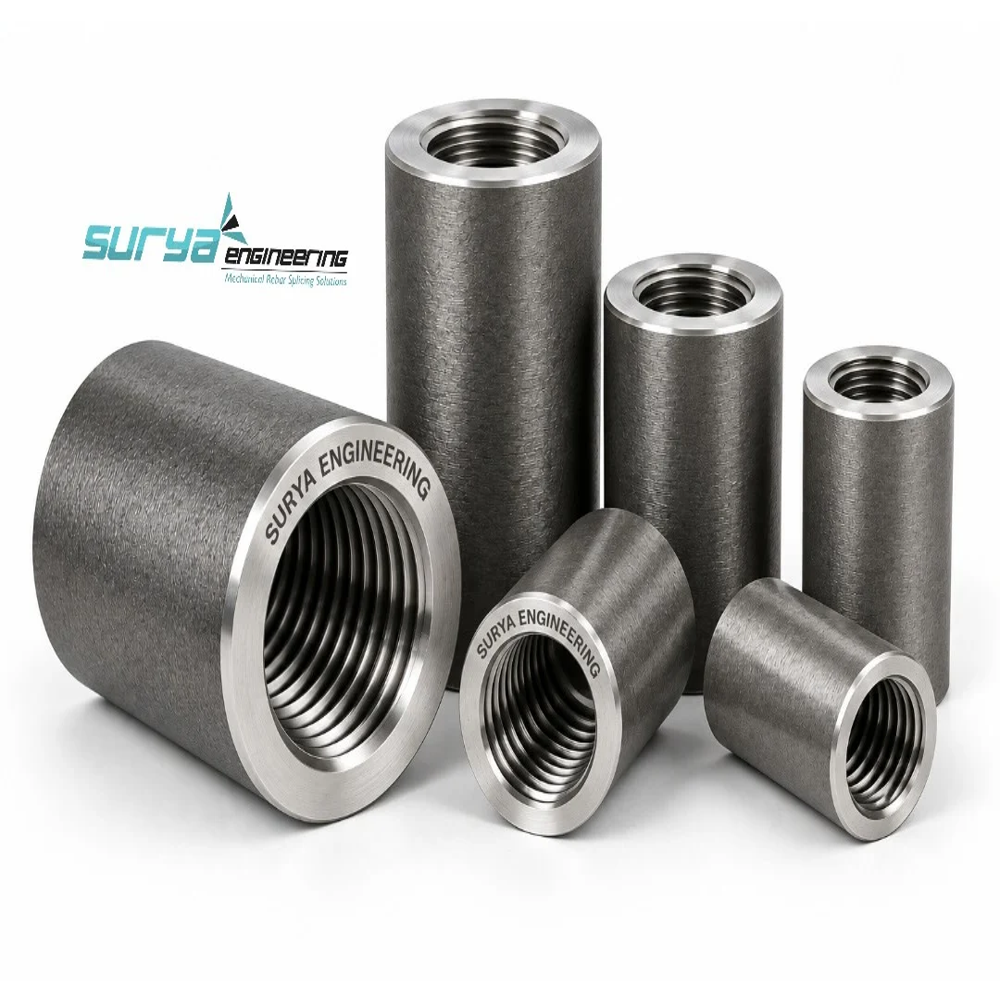
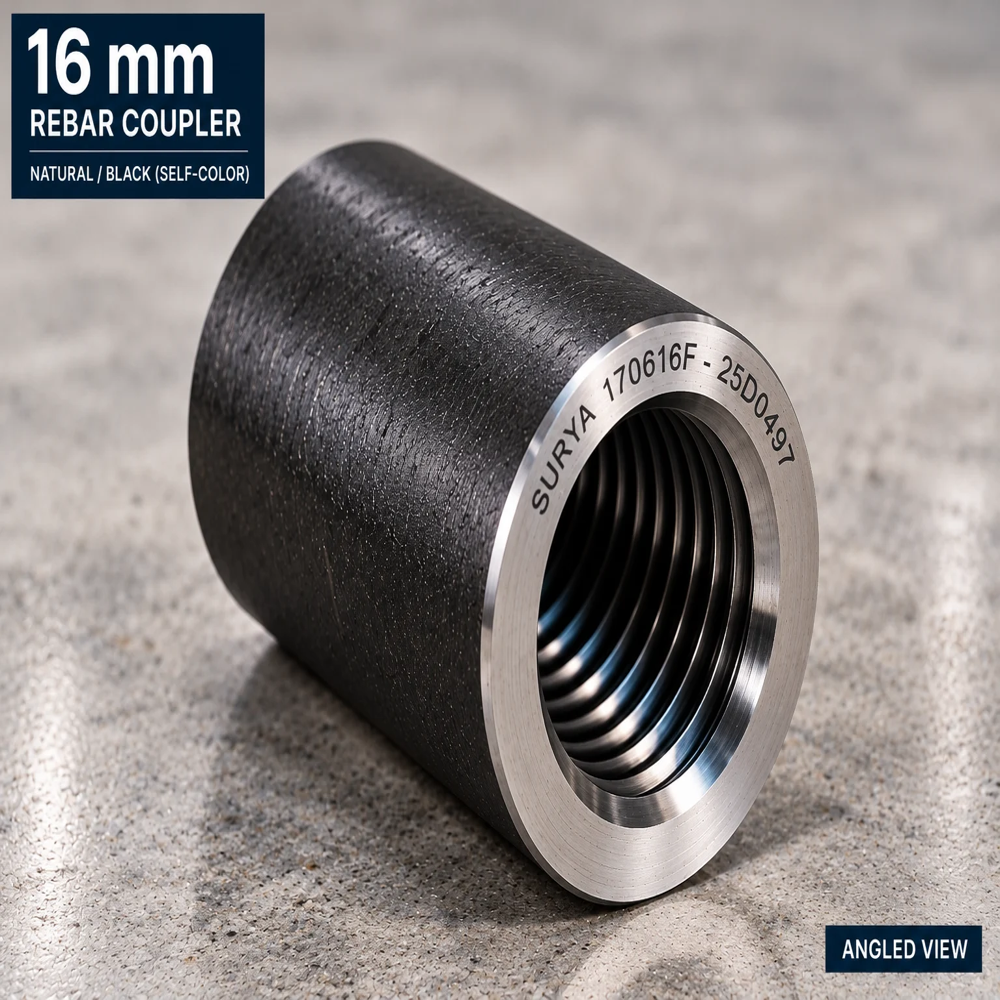
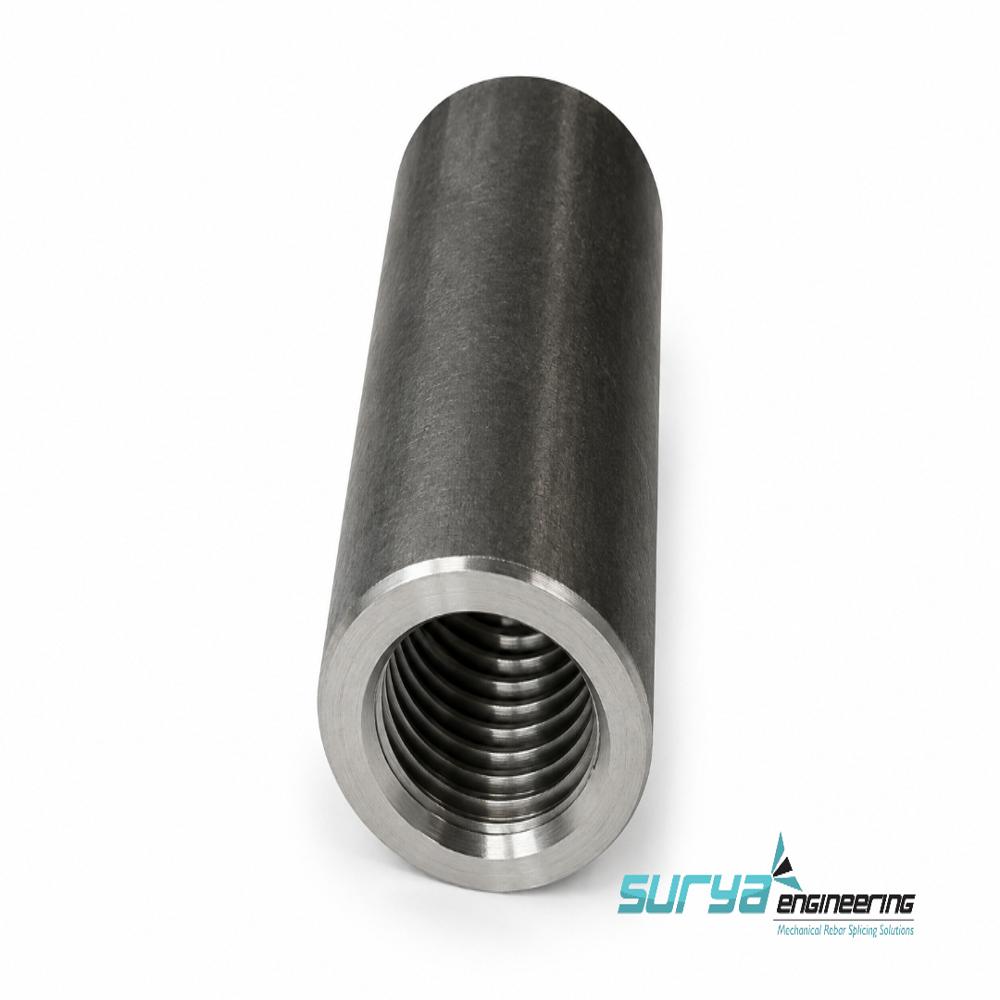
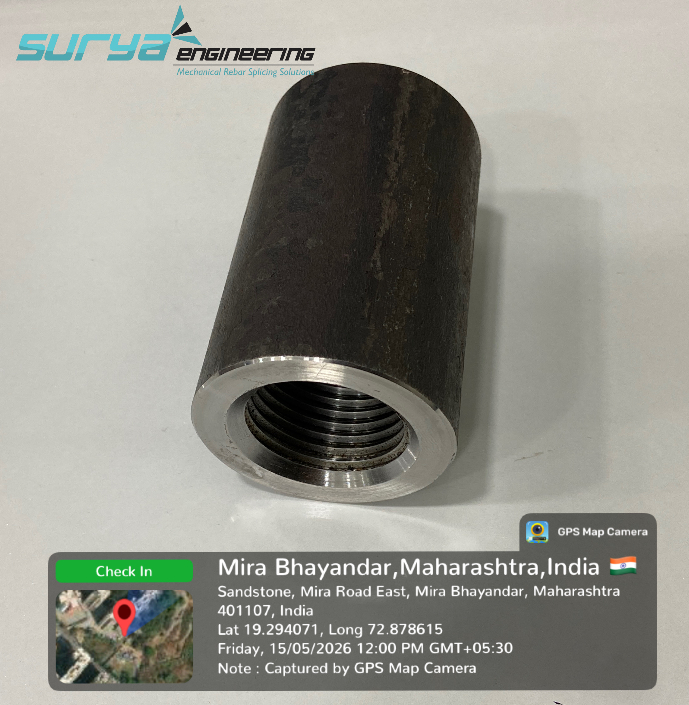
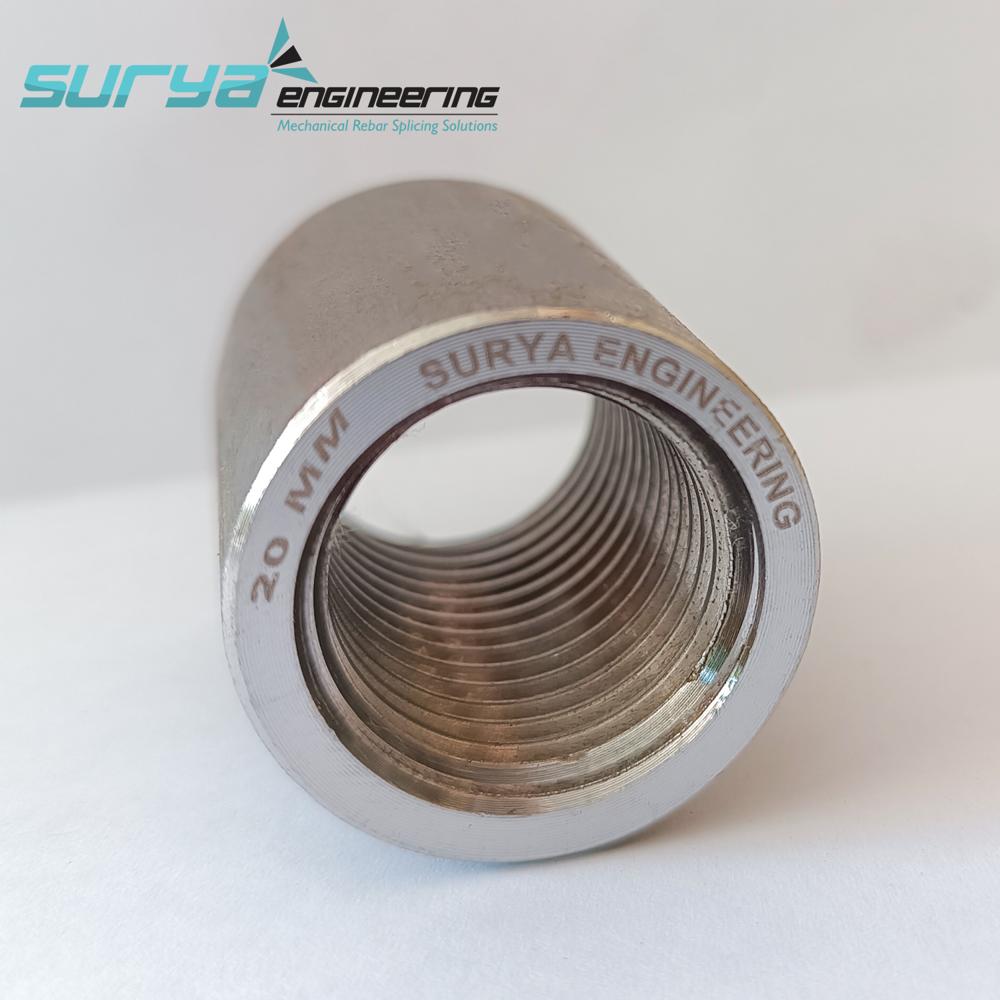
EN8D Rebar Coupler for TMT Bar Connections

EN8D Rebar Coupler for TMT Bar Connections

EN8D Rebar Coupler for TMT Bar Connections Specification

  • Constitute
  • Standard
  • Color
  • Black
  • Sleeve size
  • 16mm, 20mm, 25mm, 32mm, 40mm - To match TMT Bar
  • Weight
  • 0.18 Kg, 0.28 Kg, 0.45 Kg, 0.72 Kg, 1.10 Kg Kilograms (kg)
  • Features
  • 700-750 MPa UTS, Bar-Break Guarantee, 125% fy as per IS 16172:2023, Slip <0.10mm, Type 2 + Class L/H, Saves 15% Steel, No Welding
  • Technique
  • Forged, Welded Layher
  • Product Type
  • Cuplock System
  • Material
  • Steel
  • Components
  • Couplers
  • Diameter
  • 6mm, 20mm, 25mm, 28mm, 32mm, 36mm, 40mm Millimeter (mm)
  • Width
  • 28mm to 62mm Millimeter (mm)
  • Length
  • 55mm, 65mm, 75mm, 90mm, 110mm Millimeter (mm)
  • Thickness
  • 8mm to 15mm Millimeter (mm)
  • Surface Treatment
  • Hot Dip Galvanized
  • Application
  • Construction
  • Size
  • 16mm to 40mm
 

EN8D Rebar Coupler for TMT Bar Connections Trade Information

  • Minimum Order Quantity
  • 10 Kilograms
  • Delivery Time
  • 24 Hours
 

About EN8D Rebar Coupler for TMT Bar Connections

EN8Dl Rebar Coupler for TMT Bar Connections

What is EN8D Material?

EN8D is a medium carbon steel grade under British Standard BS970 - 080M40. It's also written as EN8Dl in market.

It's preferred for couplers because Mild Steel fails under high tensile load, while EN8D gives 650-750 MPa strength with good machinability.

Chemical Composition of EN8D:

Element
%
Carbon (C)
0.40 to 0.45%
Silicon (Si)
0.05 to 0.35%
Manganese (Mn)
0.70 to 0.90%
Sulphur (S)

<=0.06%

Phosphorus (P)

<=0.06%


 Types of EN8D Rebar Couplers

All types use same EN8D material, only thread design differs:

a) Parallel Threaded Coupler: Most common. Cold-forged, parallel threads. For standard columns/beams. Complies with IS 16172:2023, ACI 318 Type 1 & 2, BS 8110

b) Taper Threaded Coupler: Tapered threads for easy alignment, better for precast.

c) MBT / Bolted Coupler (Mechanical Bolted): No threading needed. Two TMT bars inserted and bolts tightened till shear-off. Material Grade EN8D Carbon Steel. Ideal for repair work.

d) Cold Forged / Type II Bar-Break Coupler: Bar ends are cold-forged to increase diameter before threading. No reduction in cross-section. Guarantees bar-break failure, not coupler failure.

e) Position Coupler: For places where both bars cannot be rotated.


Technical Specification - Standard Sizes

Manufactured as per IS 16172:2023


Rebar Dia
Coupler Outer Dia (OD)
Coupler Length
Thread Pitch
TMT Grade Compatible
12mm
21mm
45-50 mm
2.5 mm
Fe500 / 500D / 550
16mm
28mm
55-60 mm
3.0 mm
Fe500 / 500D / 550 / 600
20mm
32mm
65-70 mm
3.0 mm
Fe500 / 500D / 550 / 600
25mm
40mm
75-80 mm
3.0 mm
Fe500 / 500D / 550 / 600
32mm
50mm
90-95 mm
4.0 mm
Fe500 / 500D / 550
40mm
62mm
110-120 mm
4.0 mm
Fe500 / 500D

Standard Sizes are 12mm,16mm,20mm,25mm,32mm,40mm with OD ranging 21mm to 62mm.

  • Surface: Black / Self-colour / Hot Dipped Galvanized
  • Thread Type: Parallel thread (rolled or cut)
  • Tolerance: +/- 1%

How It Works - Why Better Than Lapping?

Lap splicing needs 40-60x dia overlap. For 25mm bar, that's 1 to 1.5m extra steel per joint. Coupler eliminates that.

Under IS 16172, a full-strength coupler must develop at least 125% of specified yield strength (fy) of parent bar. Failure must happen in the TMT bar, not in coupler.

Benefits:

  • Saves 10-15% steel
  • Prevents congestion, honeycombing - concrete flows easily
  • Seismic safe - tested for cyclic loading (Zone III, IV, V)
  • Faster work, no welding
  • Works where lapping impossible - piles, precast, tight formwork

Manufacturing Process at Surya Engineering

  1. Raw material check - EN8D billets test for C=0.40-0.45%
  2. Cold forging / hot forging to required OD
  3. CNC machining of internal parallel threads
  4. GO / NO-GO gauge inspection for every batch
  5. Anti-rust coating / Galvanizing

We manufacture couplers with tensile strength up to 700-750 MPa with no reduction in cross-sectional area.


Quality Testing as per IS 16172:2023

Every batch should have:

  • Static Tensile Test: UTS >= 625 MPa min, must achieve bar break
  • Slip Test: Total slip < 0.10 mm
  • Low-Cycle Fatigue: 10,000 cycles alternate tension/compression
  • High-Cycle Fatigue (for Class H): S-N curve test for bridges/towers
  • Chemical Composition Test

Applications

High-rise buildings in Mumbai/Thane, Metro projects, bridges & flyovers, dams, industrial floors, foundation piling, precast elements, seismic retrofitting.


FAQ

1. Why EN8D specifically, why not Mild Steel or EN8?
MS has UTS 410-450 MPa, it will strip before a Fe550 TMT bar yields. EN8D is 080M40 medium carbon steel with C 0.40-0.45%. That gives 650-750 MPa UTS after forging, without heat treatment. EN8 has higher sulphur, EN8D is cleaner grade - better for threading and GO/NO-GO consistency.

2. Is EN8D weldable? Can I weld a coupler to a plate?
No. At 0.40%+ carbon, Carbon Equivalent (CE) is >0.60. Welding will cause HAZ cracking. If you need weldable coupler, you need to use EN8D coupler + weldable anchor head, never weld directly on coupler body.

3. Why does the coupler have higher strength [700 MPa] than the TMT bar [550/600 MPa]?
As per IS 16172:2023, splice must develop 125% of fy of bar. Failure must be Bar-Break, not Coupler-Break. If coupler is same strength as bar, failure will be at threads. EN8D is intentionally over-strength.

4. Cut threads vs Rolled threads - which is better for fatigue?
Cut threads cut the grain flow, rolled threads form the grain flow. Rolled threads give 30-40% better fatigue life. That's why IS 16172 Class H [high-cycle for bridges] always requires rolled threads. Cut threads are only allowed for Class L.

5. Cold-forged vs Hot-forged coupler - difference in grain structure?
Cold forging enlarges bar end diameter by 15-20% before threading. So threaded cross-section is BIGGER than parent bar. No area loss. Hot-forged couplers are made from solid EN8D bar drilled and threaded - grain is discontinuous. Cold-forged gives true bar-break.

6.Can I use a standard coupler in compression? Does length change?
Coupler in compression works even better than tension. But you still need same engagement. Common mistake: contractors think compression needs less engagement and leave gap in centre. Centre gap >3mm creates eccentric load and buckling of bar ends inside coupler.


Tell us about your requirement
product

Price:

Quantity
Select Unit

  • 50
  • 100
  • 200
  • 250
  • 500
  • 1000+
Additional detail
Mobile number

Email

More Products in Rebar Coupler Category

Tmt Rebar Coupler

Tmt Rebar Coupler

Price 40.0 INR / Piece

Minimum Order Quantity : 500 Pieces

Taper Rebar Coupler

Taper Rebar Coupler

Price 50.0 INR / Piece

Minimum Order Quantity : 1000 Pieces

rebar coupler

rebar coupler

Price 80.0 INR / Piece

Minimum Order Quantity : 50 Pieces

Rebar Coupler

Rebar Coupler

Price 56.0 INR / Piece

Minimum Order Quantity : 10 Pieces


Back to top